High-Strength Fasteners
Bolts and Nuts for Steel Structure and Industrial Assembly
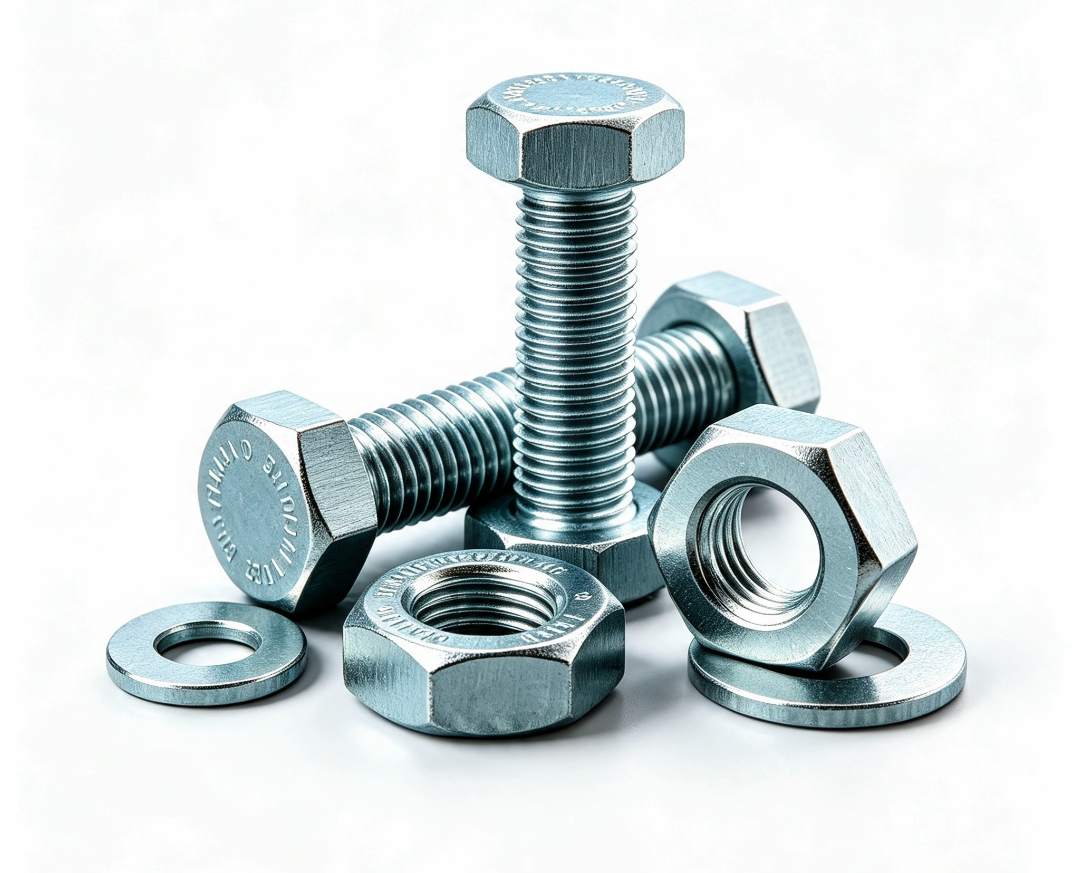
Grade 8.8, 10.9 and 12.9 high-strength bolts, nuts, washers, studs and threaded rods. DIN, ISO and ANSI standards, custom sizes to drawings, mill test certificates included.
- DIN 931 / 933
- ISO 4014 / 4017
- ANSI B18.2.1
- EN 10204 3.1
Company Strength
High-Strength Fasteners, Built for Industrial Buyers
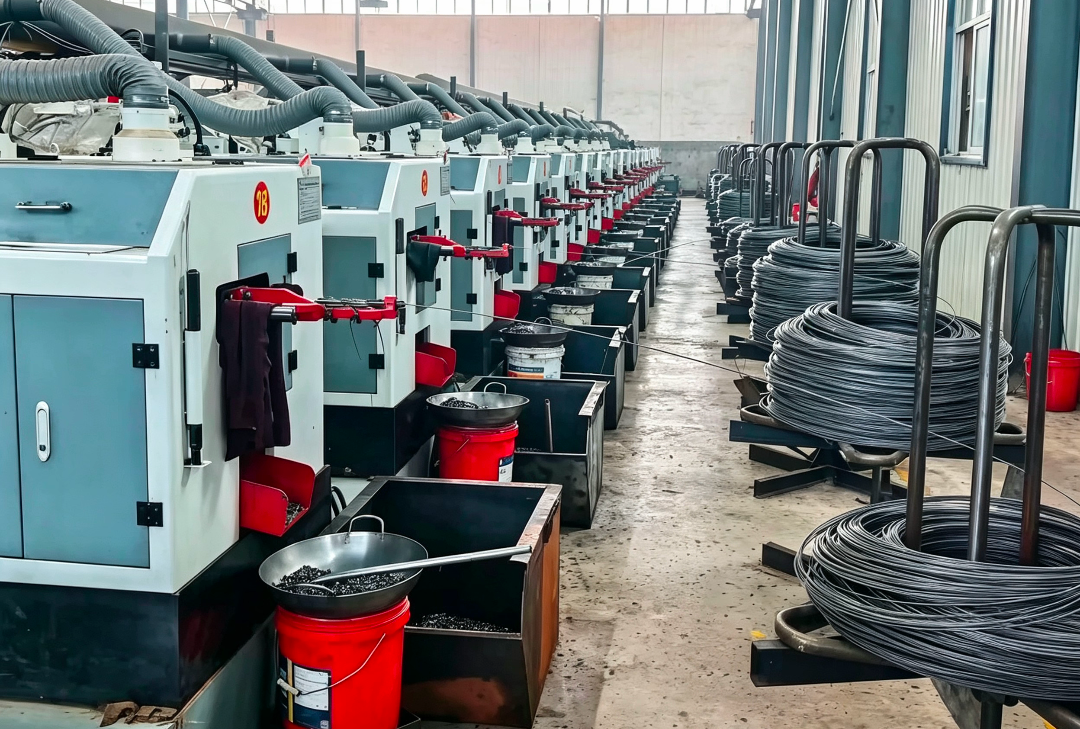
Jindai Fasteners manufactures high-strength bolts, nuts and screws for construction, machinery and infrastructure projects worldwide. Stable output, full export documentation and inspection traceability from raw material to final packing.
- 5,000tAnnual production capacity for bulk and repeat orders.
- 10+yrsExport experience in overseas industrial markets.
- 50+Cold heading and thread rolling lines for M8–M36 bolts.
- ISO 9001Certified quality system with full inspection traceability.
-
Grade 8.8 / 10.9 / 12.9
High-strength bolts produced to DIN, ISO and ANSI standards, with optional third-party tensile and hardness test reports.
- DIN 931
- ISO 4014
- ANSI B18.2.1
-
Full Product Range
Bolts, nuts, washers, expansion bolts, self-drilling screws, anchor bolts, double end studs, threaded rods and custom fasteners to drawings.
- M8–M36
- Custom
- OEM
-
Export-Ready Service
OEM and ODM support, complete export documents, and stable delivery schedules for distributors and project buyers.
- FOB / CIF
- ISPM 15
- EN 10204 3.1
-
Quality & Testing
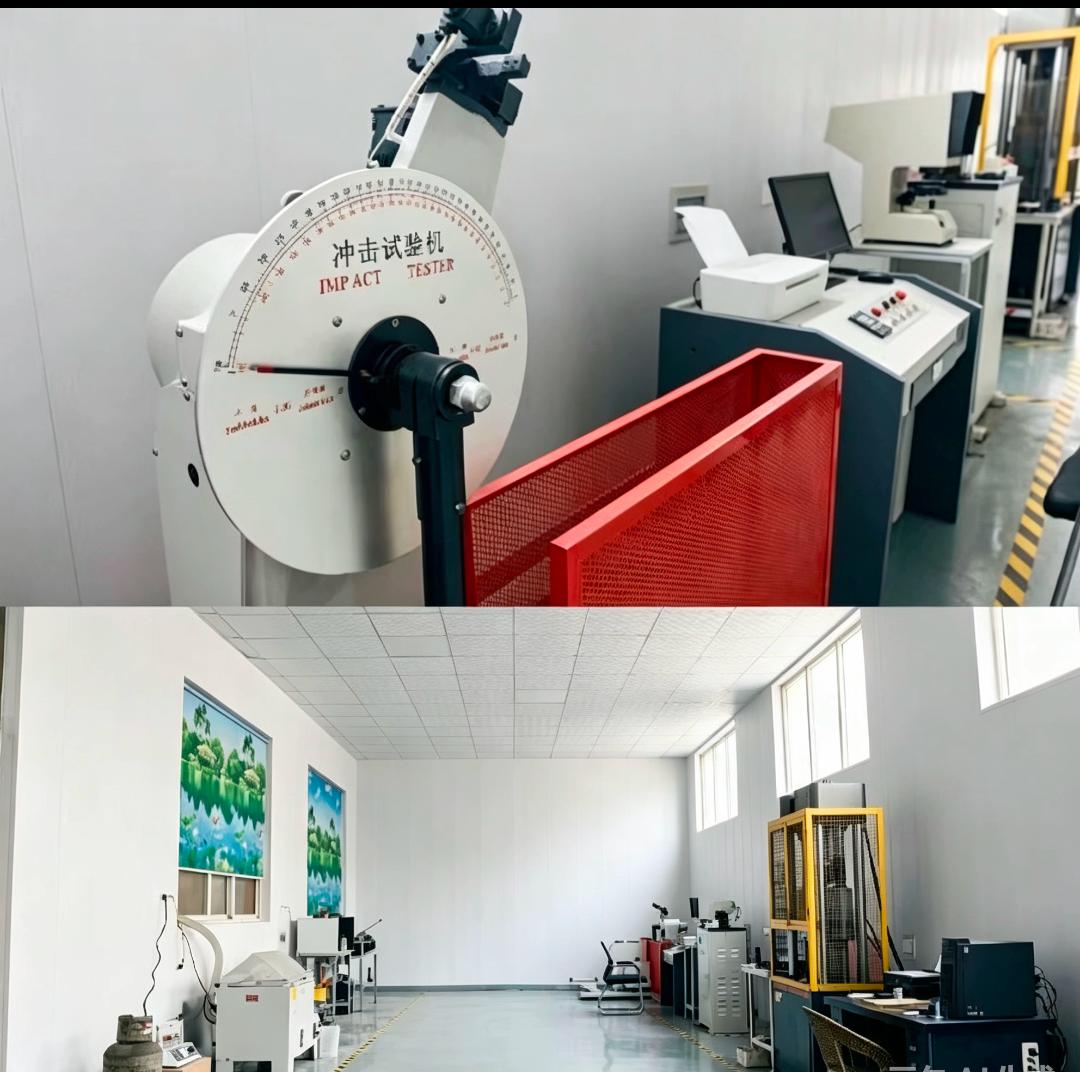
Tensile, proof load, hardness and Charpy impact testing per batch. Heat-number traceability from wire rod to finished bolt.
- Tensile
- Hardness
- Charpy
High Strength Fasteners: Bolts, Anchors & Screws
Our core fastener categories for steel structure, foundation and industrial assembly. Grades 8.8, 10.9 and 12.9; DIN, ISO and ANSI standards; custom sizes to drawings.
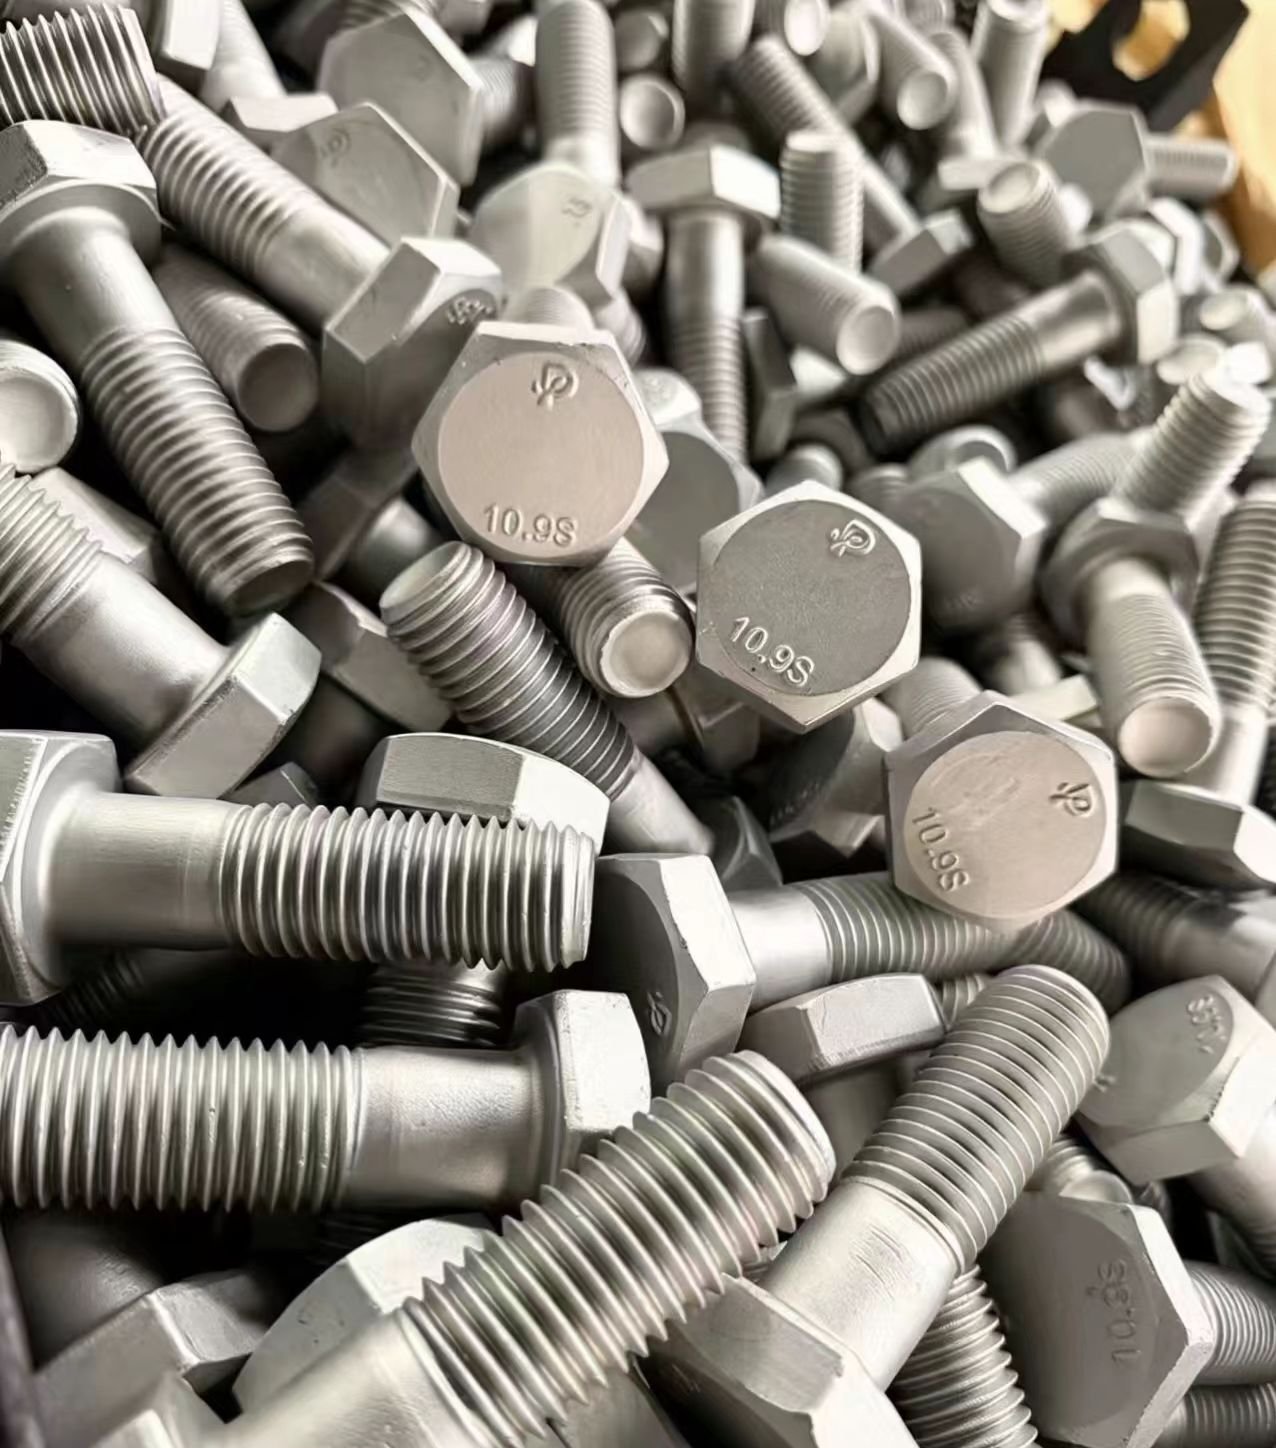
High Strength Bolts
Grade 8.8 / 10.9 / 12.9 for heavy-duty steel connections.
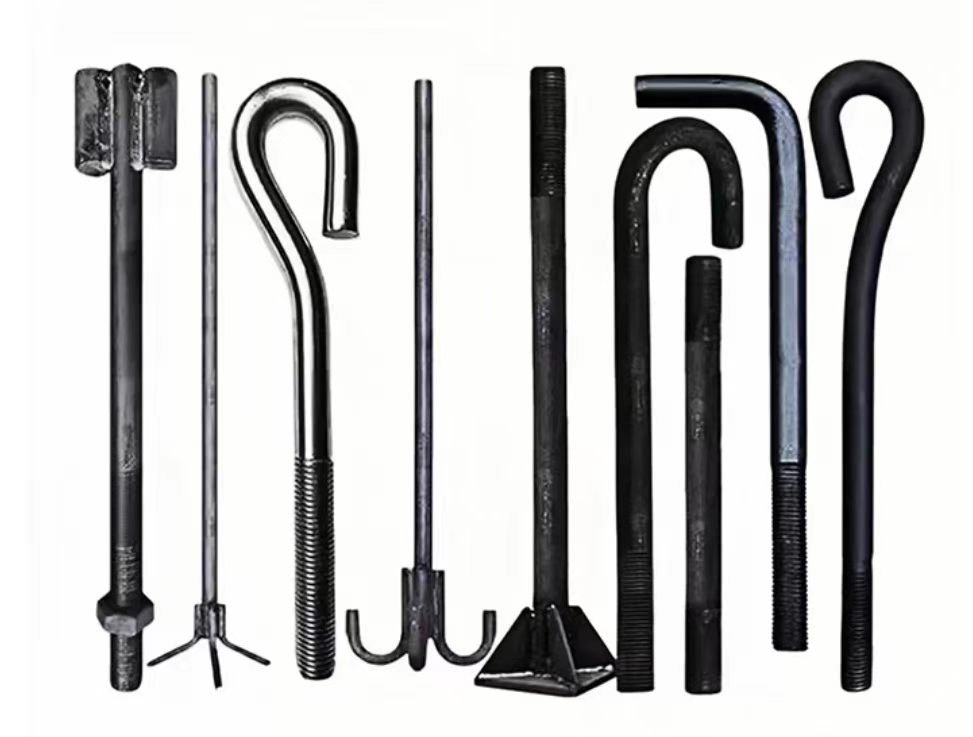
Foundation Anchor Bolts
J-type and L-type anchor bolts for foundation and base plates.
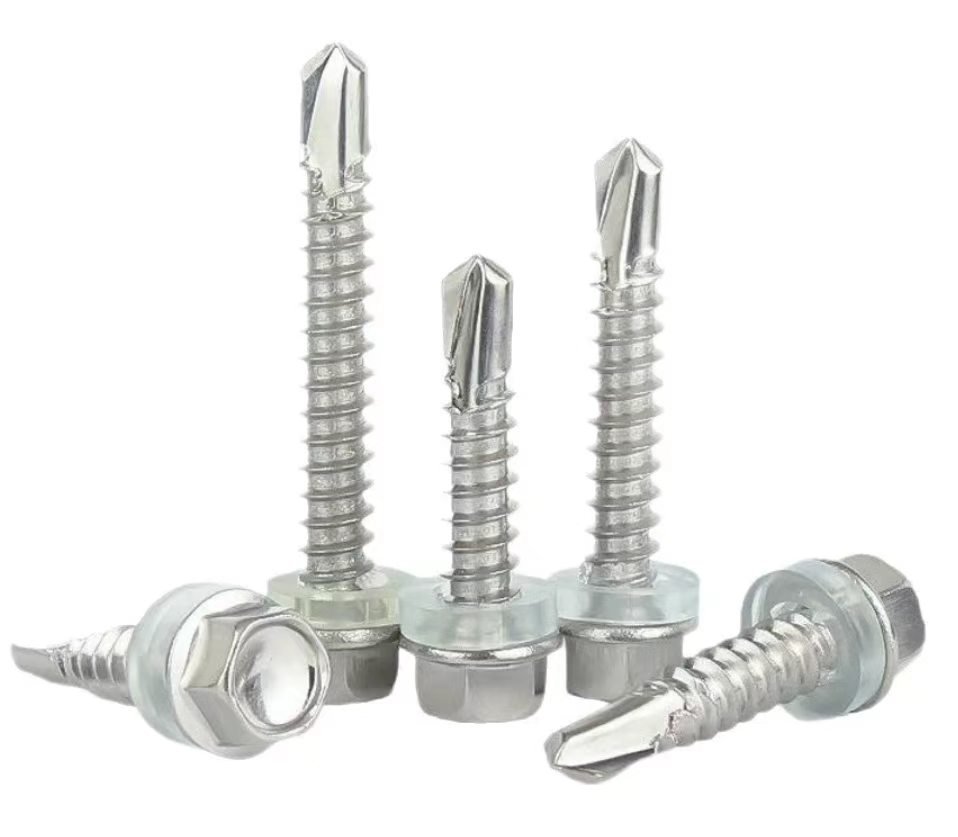
Self-Drilling Screws
Drill, tap and fasten in one step for steel and light sections.
View All Product Categories
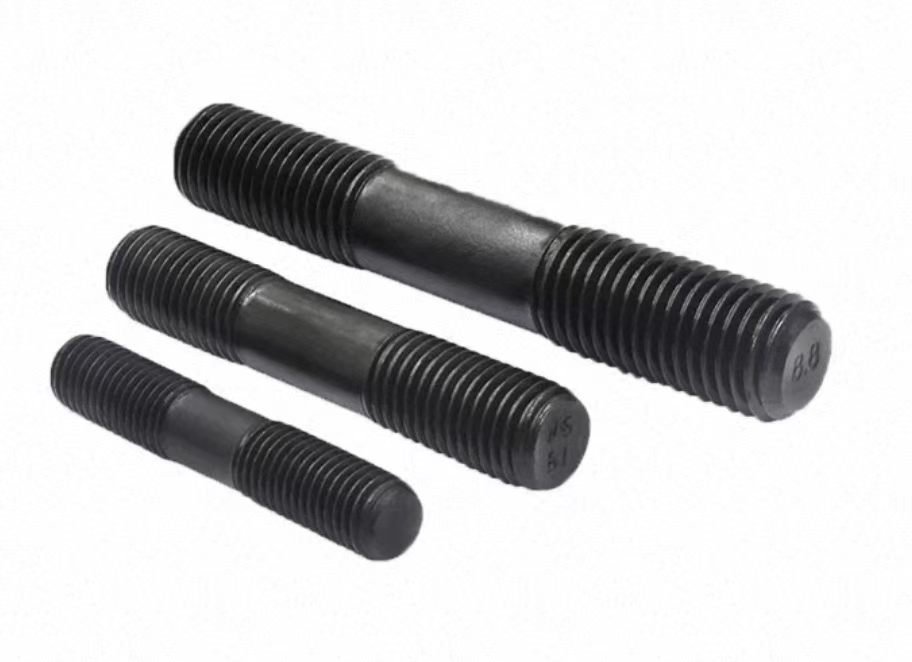
Double End Studs
Threaded both ends for flange and equipment assembly.
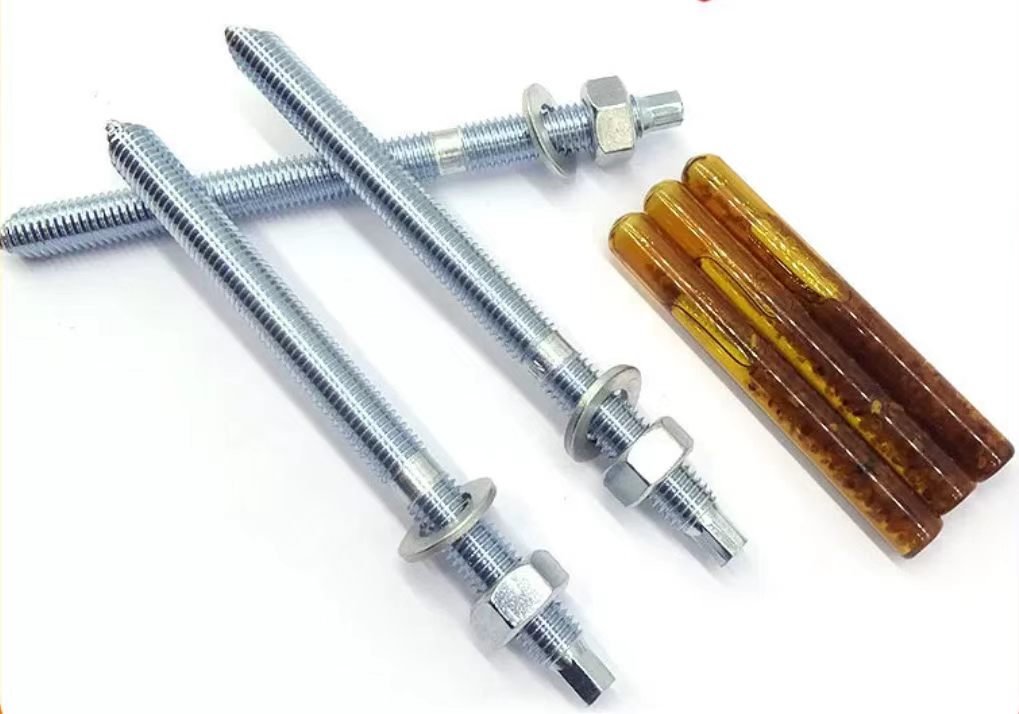
Chemical Anchors
Resin capsule anchoring for cracked and non-cracked concrete.
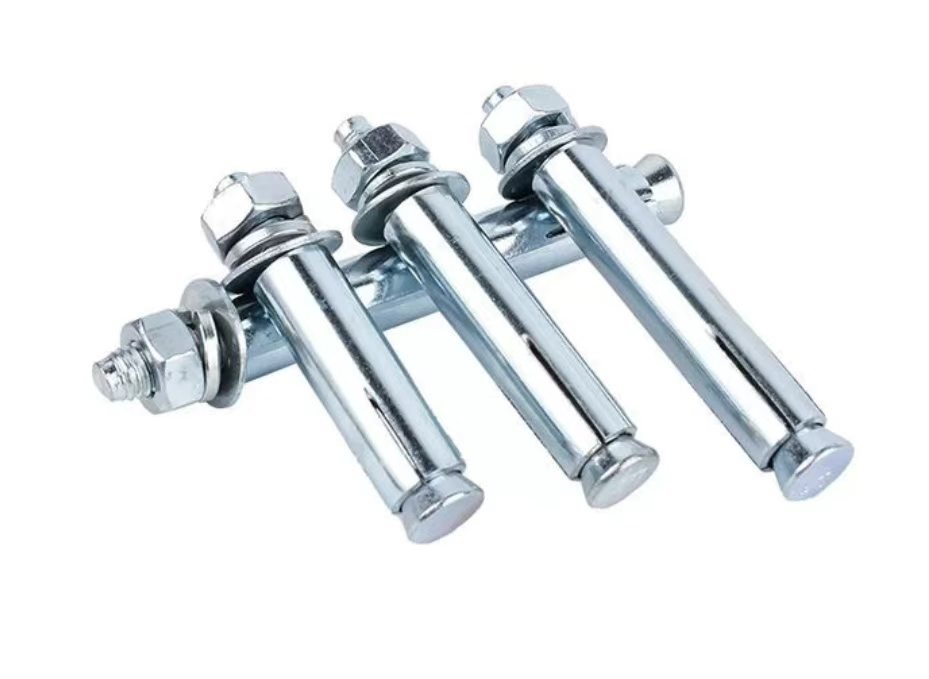
Expansion Bolts
Mechanical expansion anchoring for concrete and masonry.
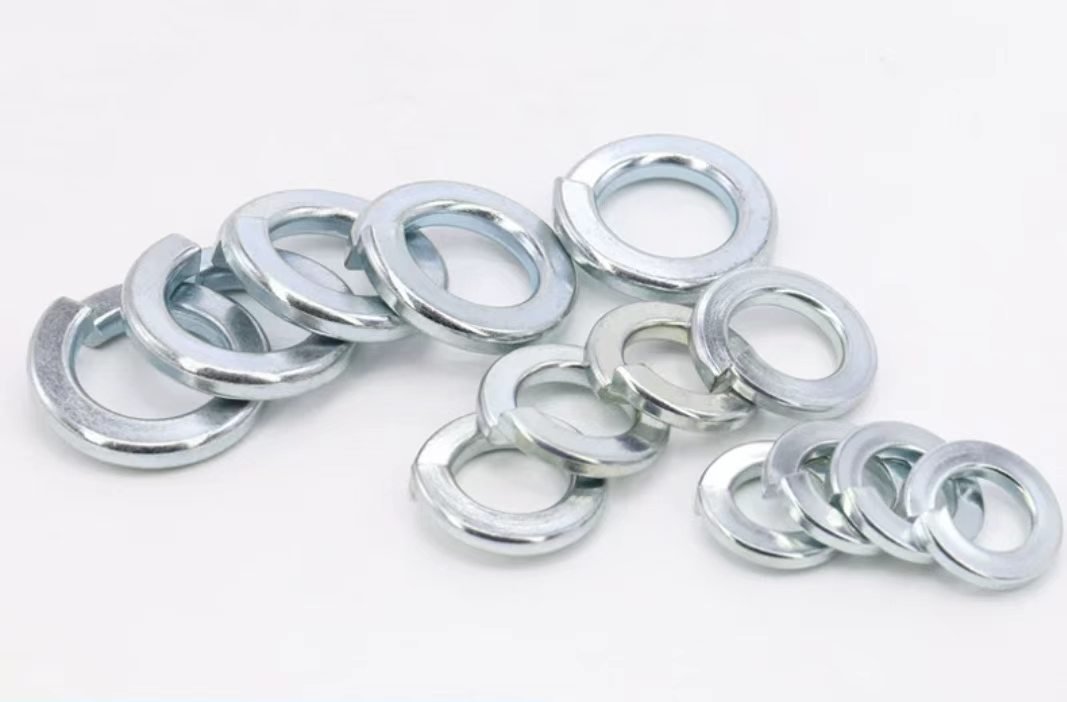
High Strength Flat & Spring Washers
Flat and spring washers matched to bolt grade and load.
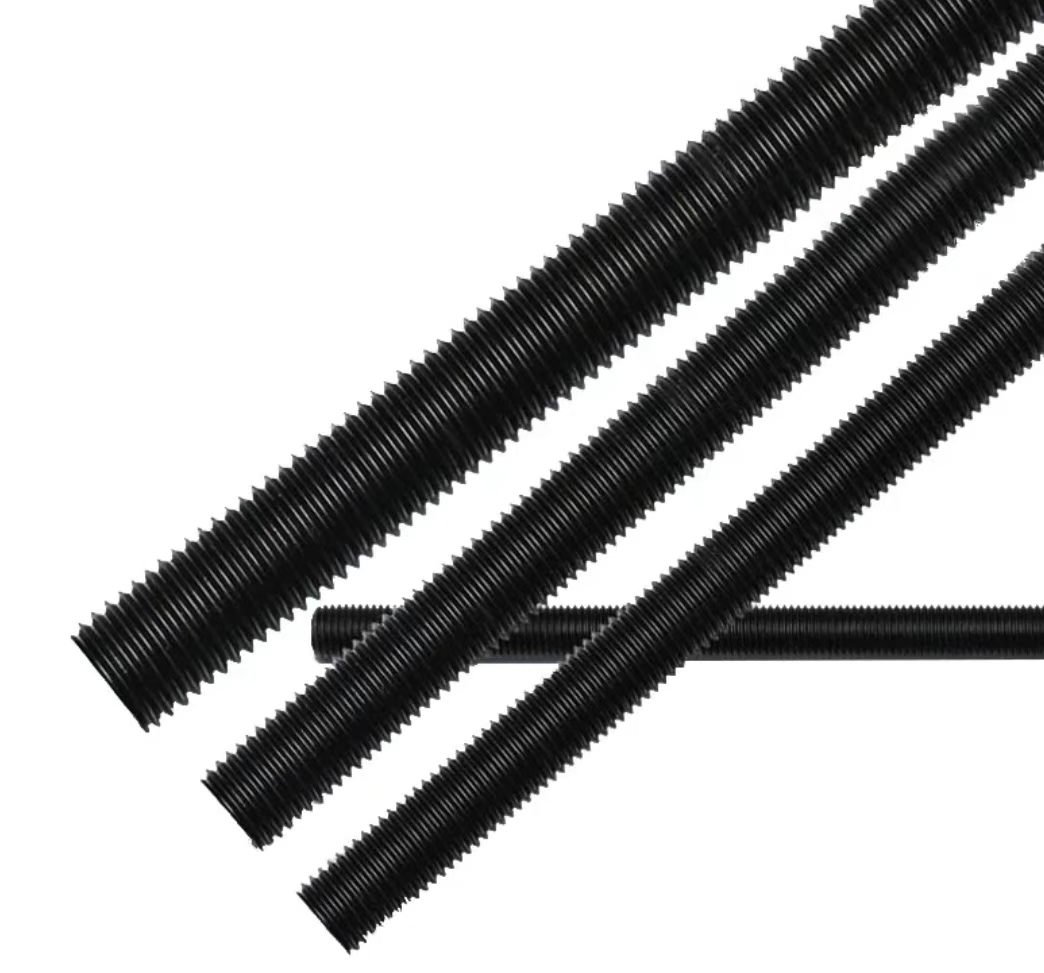
High Strength Threaded Rods
Continuous thread rods in Grade 8.8, 10.9 and 12.9.
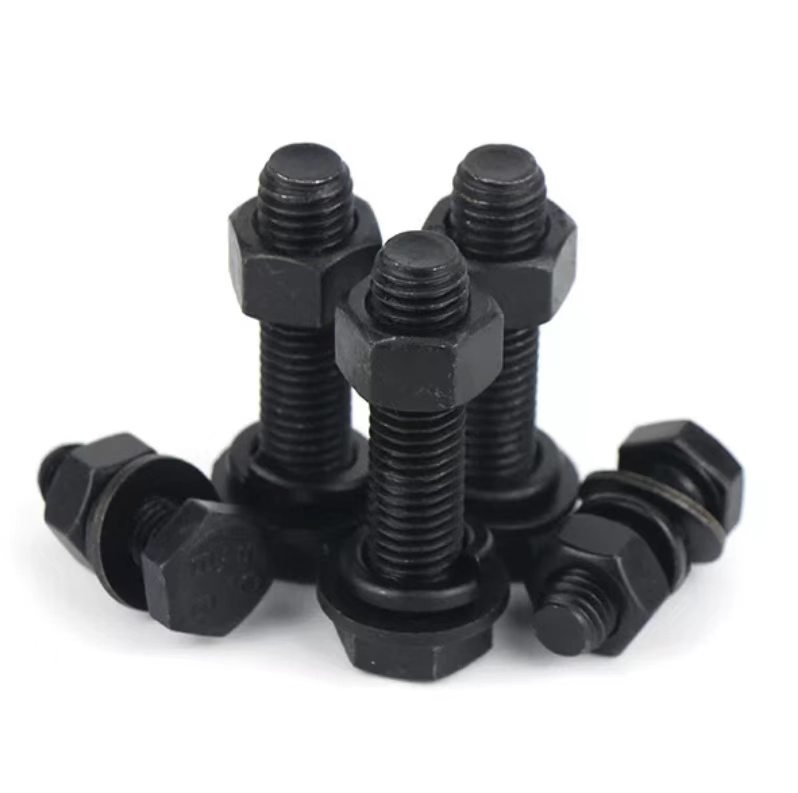
Steel Structure Bolts
HSFG and tension control bolts for steel structure joints.
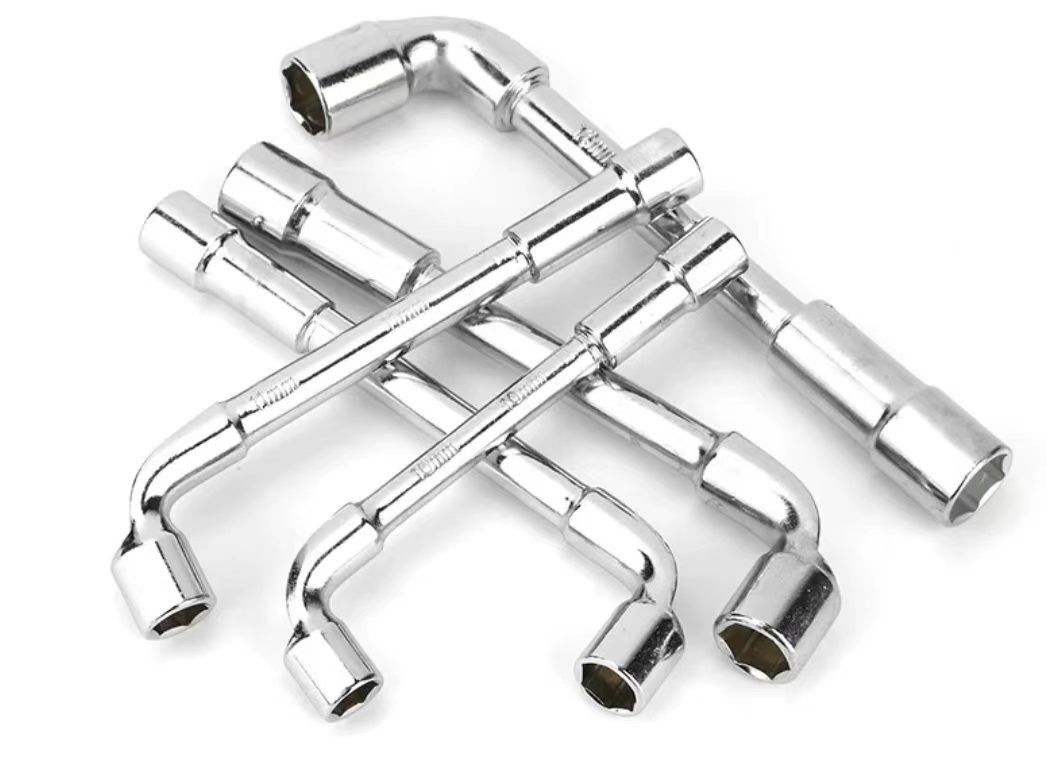
Matching Fastening Tools & Accessories
Installation tools and accessories matched to bolt and anchor systems.
Engineered for Strength.
Manufactured for Scale.
We own and operate our manufacturing facility in Yongnian, China. From raw wire rod to finished high-strength bolts (Grade 8.8, 10.9, 12.9), every process is controlled in-house with full traceability.
50+
Heading Lines
2000t
Monthly Output
100%
Batch Tested
Where High-Strength Bolts Are Used
Typical applications, with the connection parts and bolt types commonly specified in each.
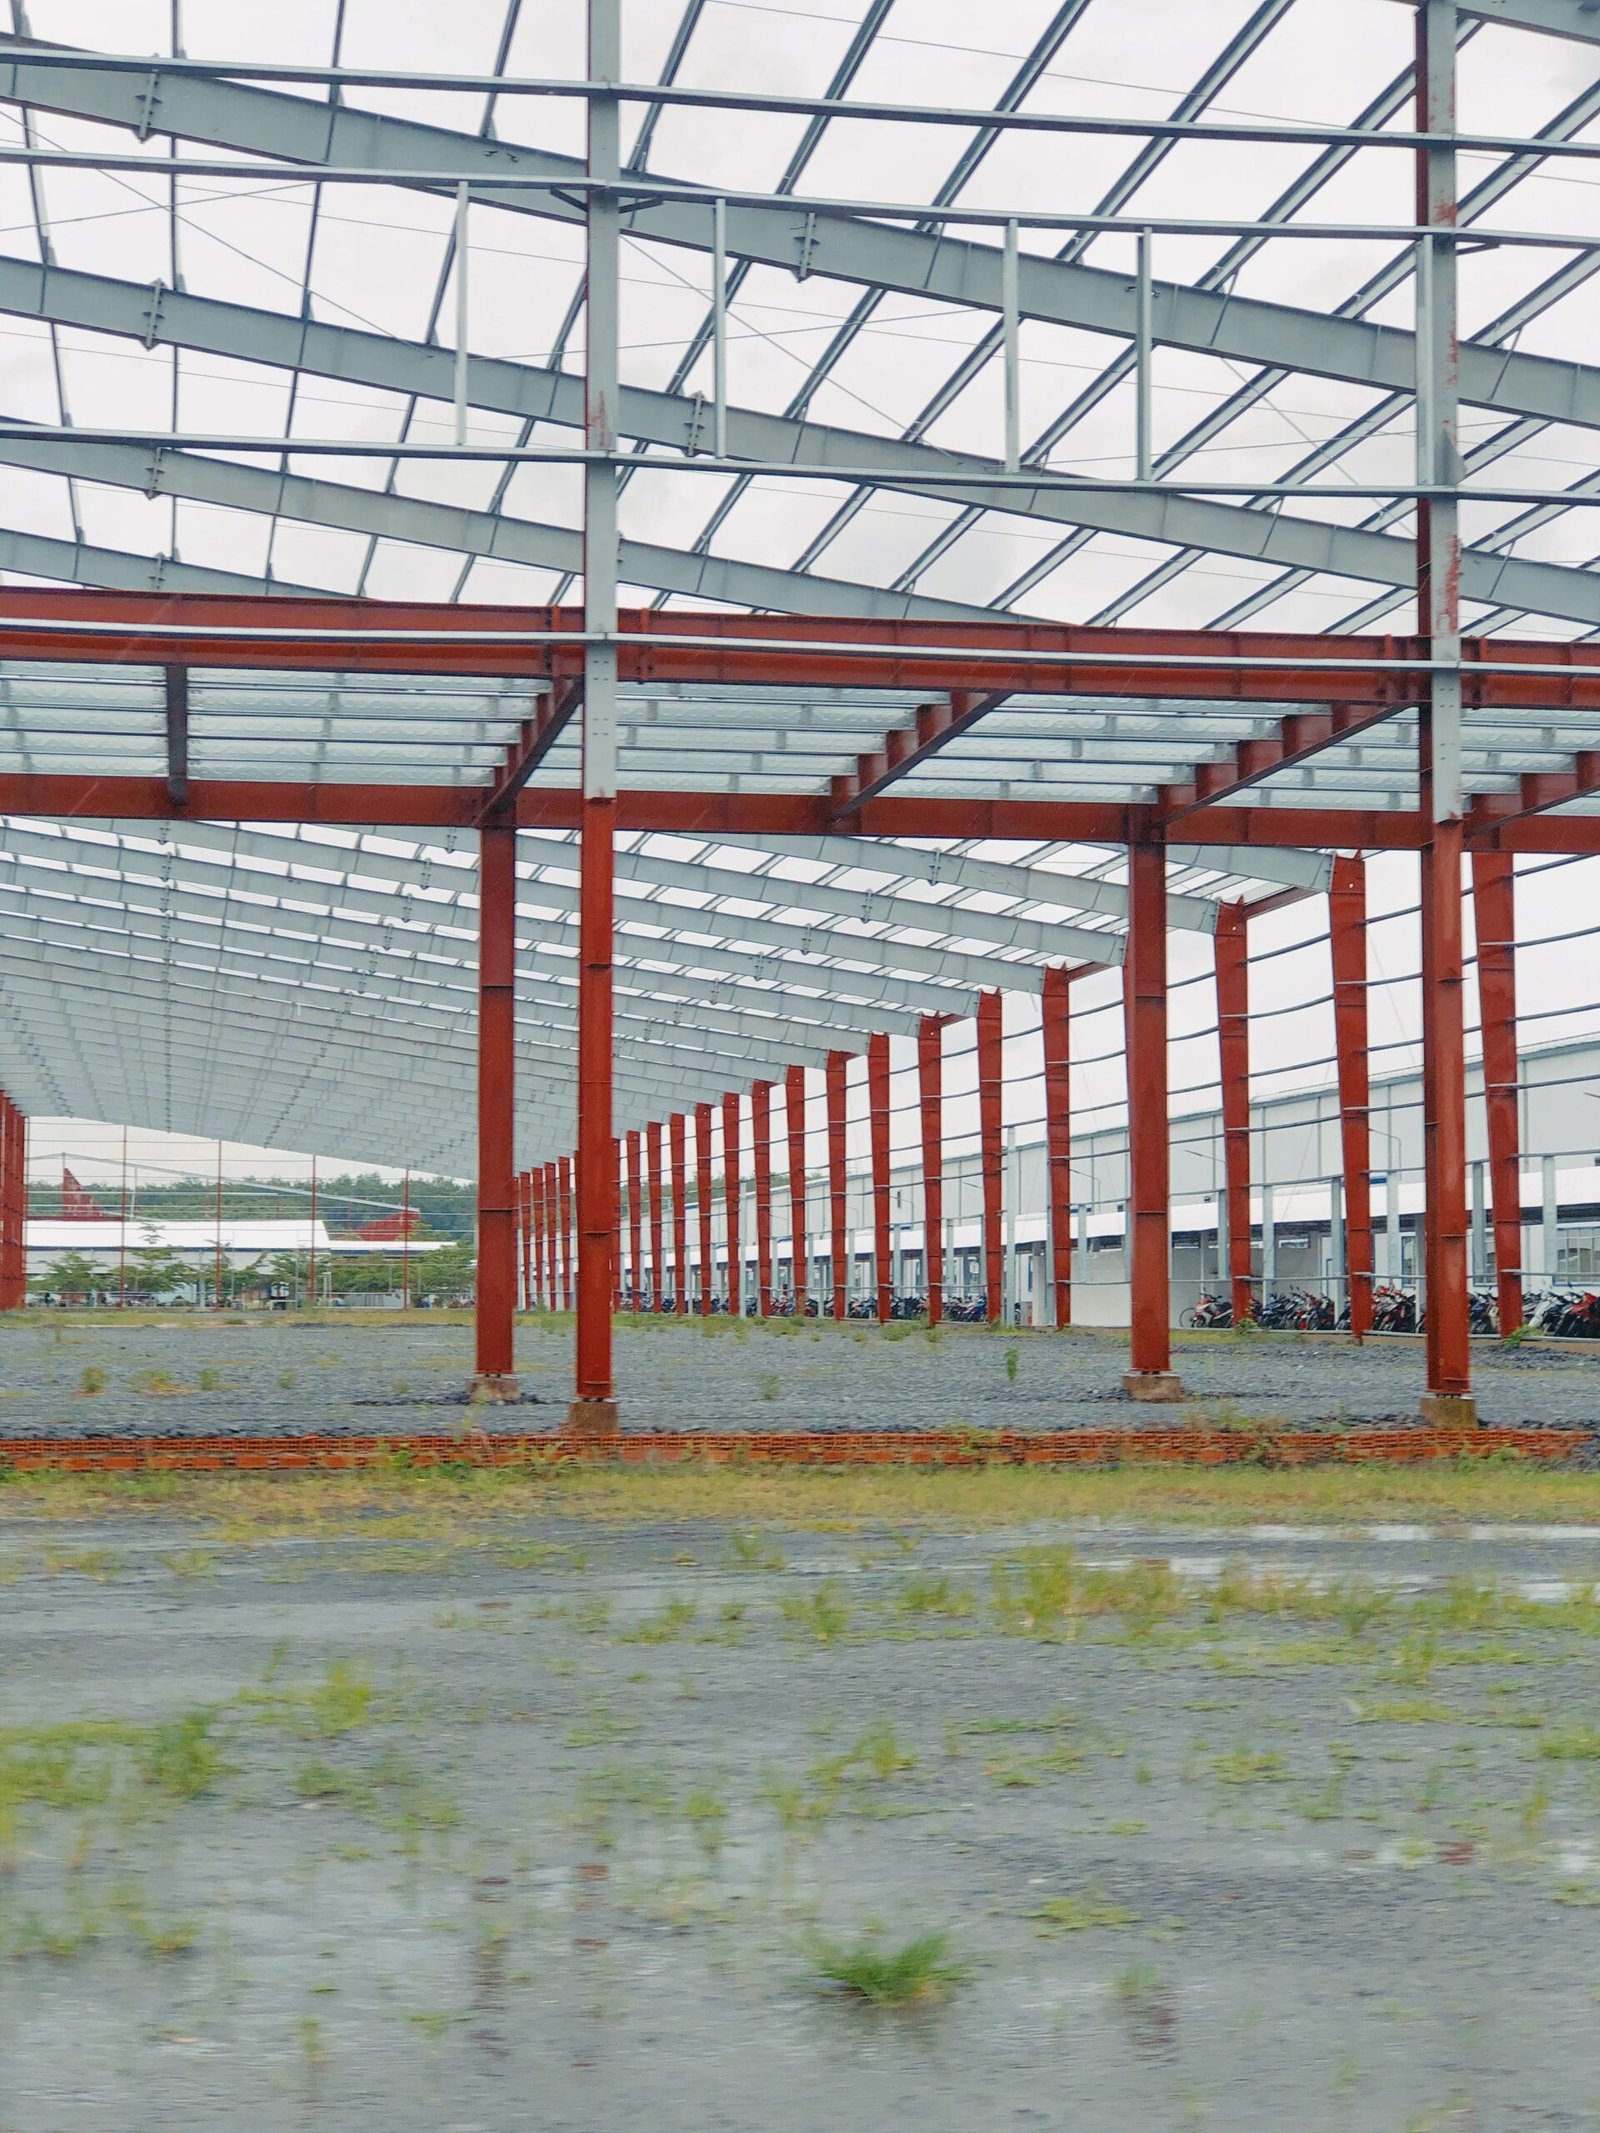
Steel Structure Plant Buildings
Beam-to-column joints, column splices and roof truss connections in industrial workshops and warehouses. Friction-grip preload is the key control point.
- Grade 10.9
- HSFG
- DIN 6914

Machinery and Equipment
Frame, axle and suspension connections under vibration and dynamic load. Controlled torque and fatigue resistance are required.
- Grade 10.9
- Flange bolt
- ISO 4162

Pipeline Engineering
Flange joints and support skids in process piping, where joint tightness and uniform preload matter.
- Grade 8.8
- Stud + nut
- ASME B18.2.1

Rail Transit
Track components and undercarriage fastening, where vibration loosening is the main concern.
- Grade 8.8
- Lock nut
- EN 14399

Wind Energy
Tower section and nacelle flange connections, exposed to wind fatigue and outdoor corrosion.
- Grade 10.9
- Hot-dip galvanized
- EN 14399

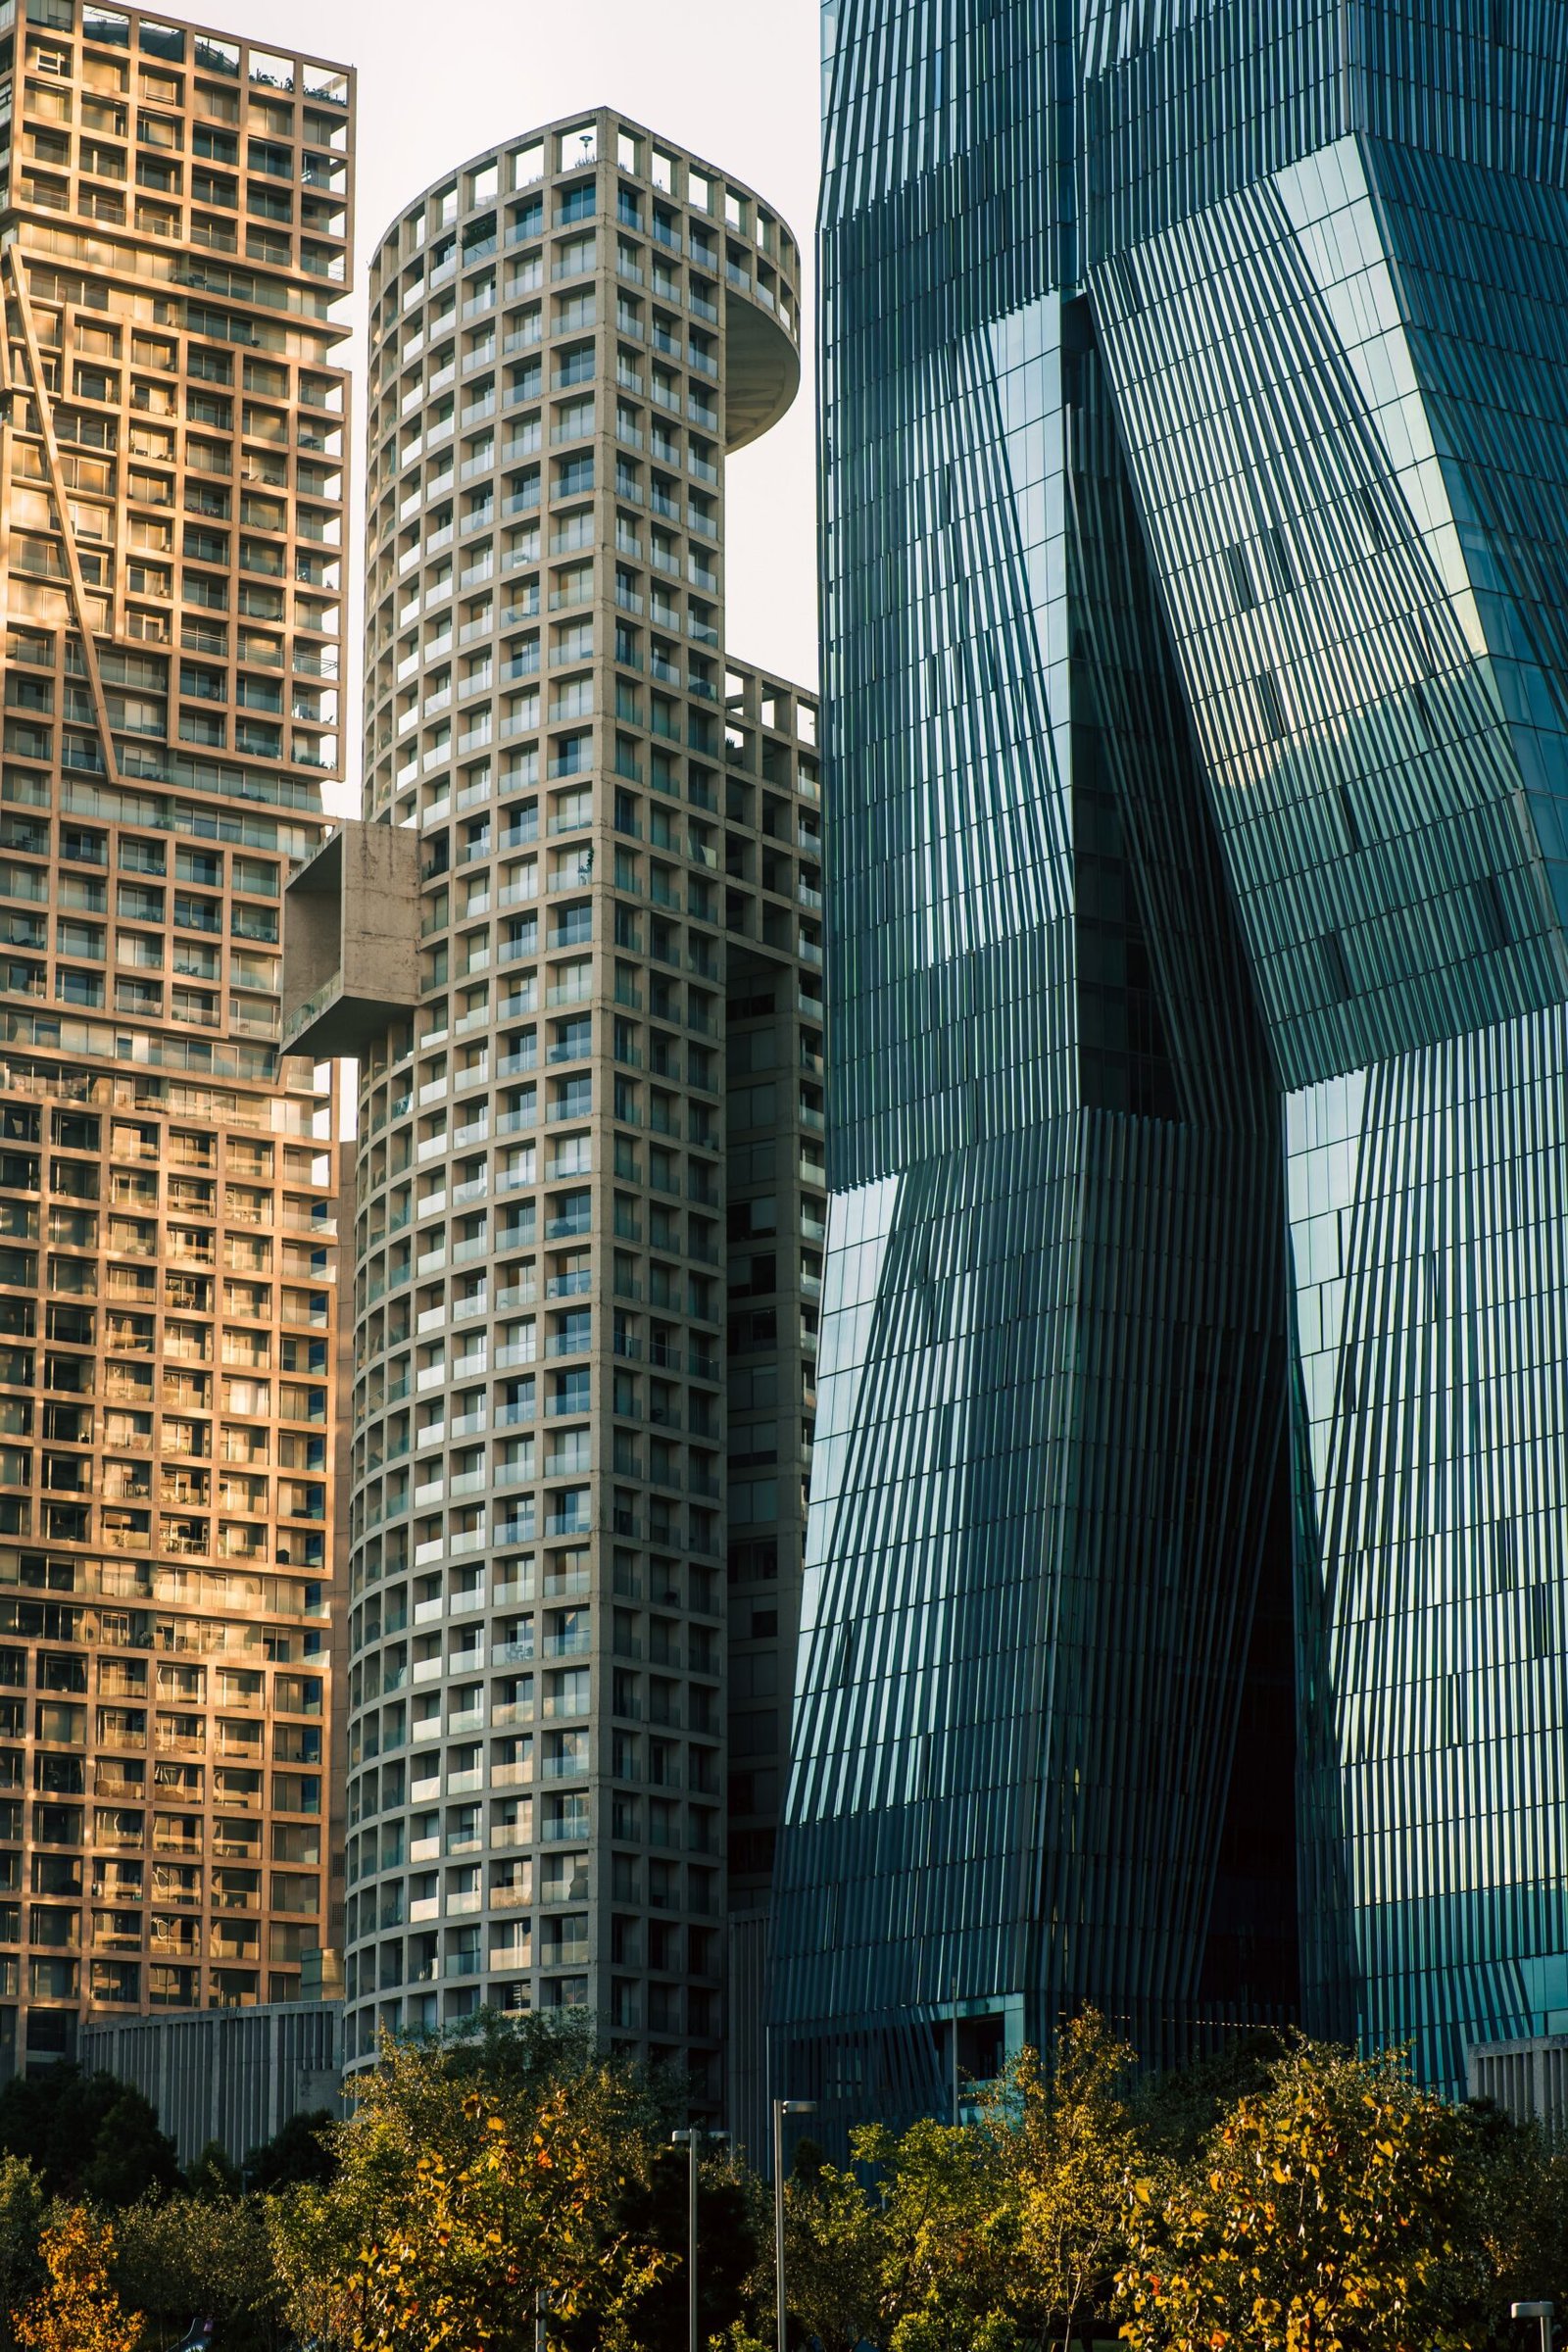
Curtain Wall and Facade
Mullion, transom and bracket connections in glass curtain wall systems, with stainless or coated fasteners for outdoor exposure.
- A2-70 / A4-80
- Stainless
- EN 1993-1-4

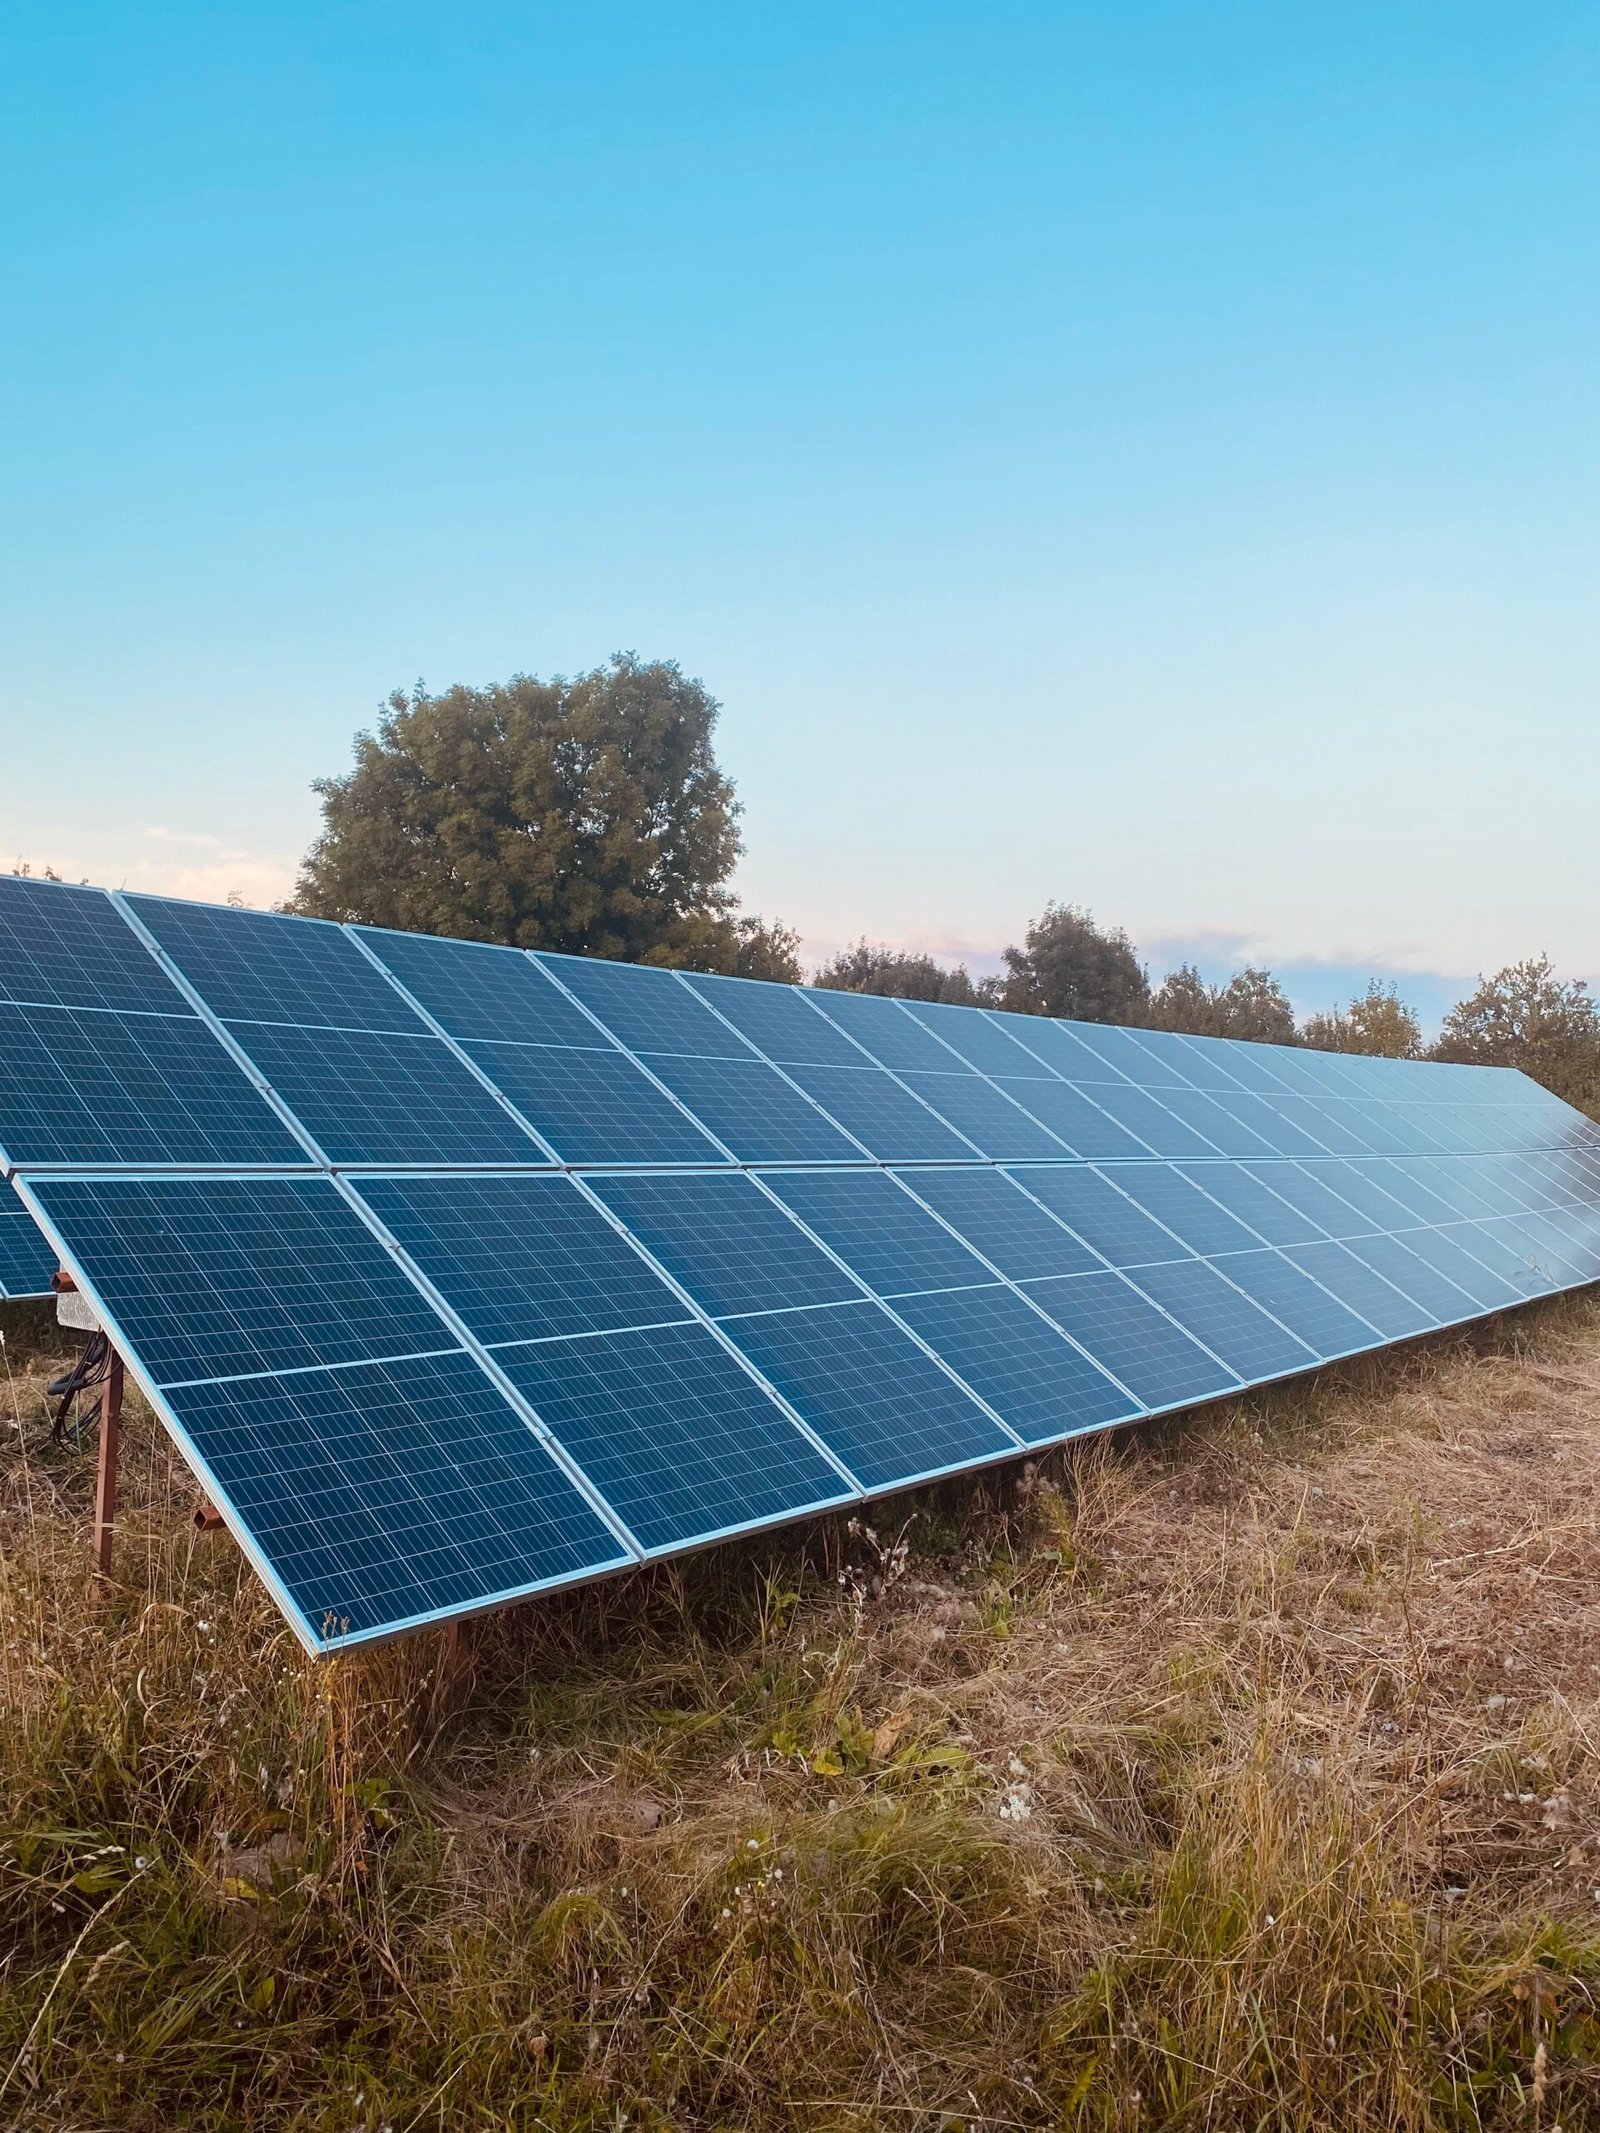
New Energy: Solar & Transmission Towers
PV mounting structures, tracker frames and transmission tower joints. Hot-dip galvanized fasteners for long-term outdoor exposure.
- Grade 8.8
- Hot-dip galvanized
- ISO 898-1

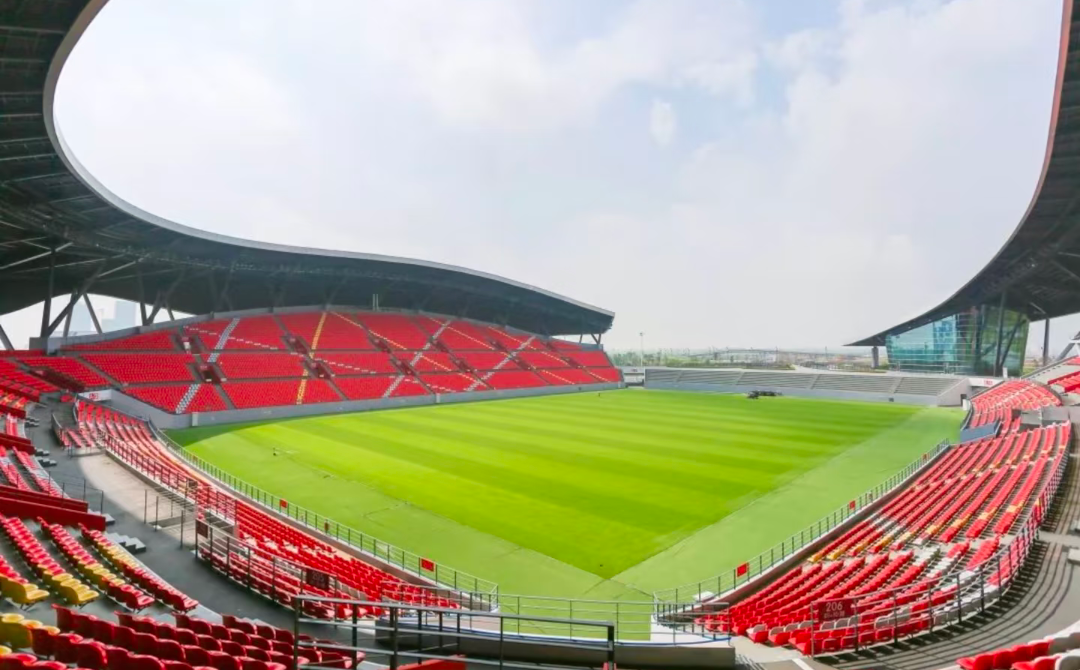
Sports Stadiums & Large-Span Buildings
Long-span roof trusses, cable-net joints and steel connection nodes in stadiums and exhibition halls, where high preload and fatigue performance are critical.
- Grade 10.9
- HSFG
- EN 14399-4
Quality Control and Test Reports
Each production batch is checked before packing. Test reports are issued with the shipment and can be shared before order confirmation on request.
ISO 9001 Quality System
Production follows a documented quality management system, covering incoming wire rod, heading, heat treatment, surface finishing and final inspection.
Mechanical Test Reports
Test reports are issued per batch for the properties that matter to the ordered grade:
- Tensile strength and proof load
- Hardness (core and surface)
- Charpy impact at low temperature
- Salt spray hours for coated parts
Batch Traceability
Heat number is recorded from wire rod to finished bolt. If a customer needs to check a specific batch, the production record and test report can be matched by heat number.
Before ordering: tell us the grade, standard and surface treatment, and we will confirm which test items apply and what the report will include.
Grade 8.8 / 10.9 / 12.9 — Mechanical Properties & Material
Values per ISO 898-1 and GB/T 3098.1, coarse thread. Material grades are typical production selections; final choice depends on diameter and inspection requirements.
| Property | 8.8 | 10.9 | 12.9 |
|---|---|---|---|
| Material grade | 35K / 45# medium carbon steel, quenched and tempered | 40Cr alloy steel, quenched and tempered | 35CrMo / 40Cr alloy steel, quenched and tempered |
| Min. tensile strength | 800 / 830 MPa M5–M16 / M18–M39 | 1040 MPa | 1220 MPa |
| Min. yield strength | 640 / 660 MPa M5–M16 / M18–M39 | 940 MPa | 1100 MPa |
| Min. proof strength | 580 / 600 MPa M5–M16 / M18–M39 | 830 MPa | 970 MPa |
| Hardness (core) | HRC 22–32 / 23–34 | HRC 32–39 | HRC 39–44 |
| Surface treatment | Black oxide, electro-galvanized, hot-dip galvanized | Black oxide, electro-galvanized (baking after plating), zinc flake | Zinc flake preferred; electro-galvanized only with baking and hydrogen embrittlement test |
| Typical use | Steel structure, machinery frames | Heavy machinery, chassis, high-preload joints | Critical joints with space and weight limits |
Note: For 10.9 and 12.9, electroplating introduces hydrogen; baking within 4 hours after plating is required. For 12.9 used in safety-critical joints, zinc flake coating is preferred over electroplating.
Frequently Asked Questions
Order-related questions from industrial buyers, answered with the numbers and limits we work to.
What is the MOQ for standard high-strength bolts?
For M8 to M24 standard sizes, MOQ is usually 500 pcs per size and grade. For M27 to M36, 200 pcs per size. Mixed sizes in one order are acceptable if each size meets its own minimum.
Can grade 12.9 bolts be electro-galvanized?
Electro-galvanizing on grade 12.9 is possible only with baking within 4 hours after plating and a hydrogen embrittlement test. For safety-critical joints we recommend zinc flake coating instead, which avoids the hydrogen risk at HRC 39-44.
What does your test report include?
Each batch report includes chemical composition of the heat, tensile strength, proof load, hardness (core and surface) and Charpy impact where required. Salt spray hours are reported separately for coated parts. Reports are matched to the heat number on the packing list.
Can you match a specific standard or drawing?
Yes. We produce to DIN 931, DIN 933, ISO 4014, ISO 4017, ANSI B18.2.1 and customer drawings. For non-standard thread, head mark or length, send the drawing with tolerance and surface requirement before quotation.
What is the lead time for 10.9 and 12.9 grades?
Stock sizes of 10.9 and 12.9 ship in 10 to 15 days. Production orders of 20 to 30 days depend on heat treatment batch schedule. Custom sizes that need new tooling add 15 to 20 days for tooling and first article approval.
How are bolts packed for sea freight?
Standard export is ISPM 15 wooden crate or pallet, inner VCI film and desiccant. Carton size, label format and pallet height can be adjusted to the customer’s warehouse or project site requirement.
Contact us
Request a Quote
For grade 8.8, 10.9 and 12.9 bolts, include diameter, length, standard and quantity. Drawings and test requirements can be sent by email after first contact.
Prefer to chat? Send your drawing or specification directly on WhatsApp and we will reply from the sales team.